Capping Machinery for packaging automation projects.
Screw, trigger, pump, crimp, ROPP, T-cork, crown and vacuum capping machinery for bottles and jars.
How this range is specified
The best machine configuration depends on product behaviour, container format, required speed, accuracy, utilities and integration requirements.
- Confirm product and pack samples before final selection.
- Review throughput expectations and operator involvement.
- Consider upstream feeding, downstream coding and conveyor transfer.
10 machinery options.
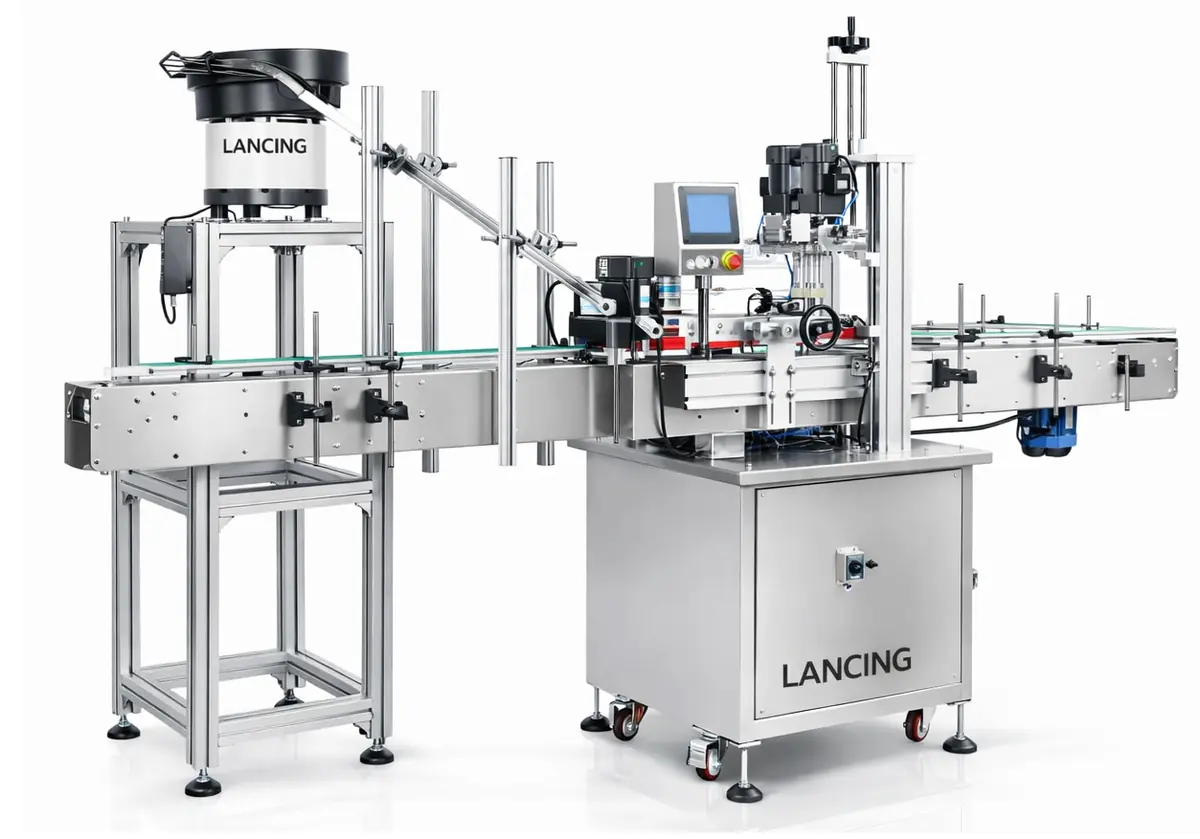
The machine-card images below are category illustrations, not verified photographs of the exact models. Ask Lancing UK to confirm model imagery and the final supplied configuration.
8-Head Rotary Capping Machine
LU-XG446Q rotary capper with eight capping heads. Confirm cap and bottle formats, torque requirements and line handling.
View machine →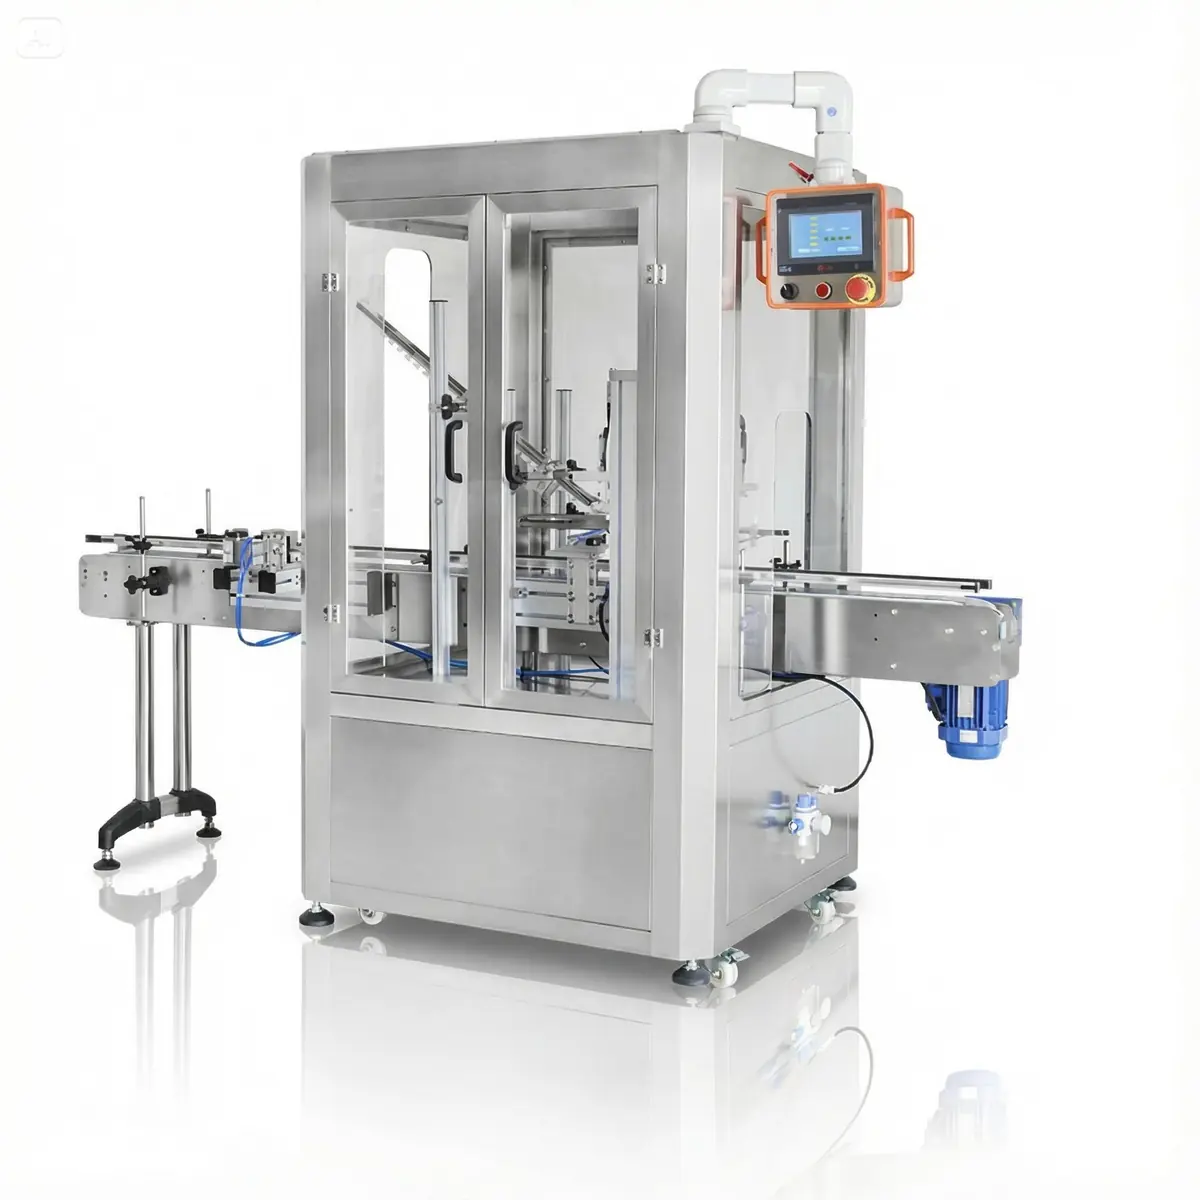
Automatic Cork Pressing Capping Machine
LU-XG16D cork feeding and pressing machine with a dust cover. Confirm the cork, bottle neck, seating and cleaning requirements.
View machine →Automatic High-Speed Capping Machine
LU-FXZ101 automatic capper with six rotary rubber wheels. Confirm the actual bottle and cap before defining the closing setup.
View machine →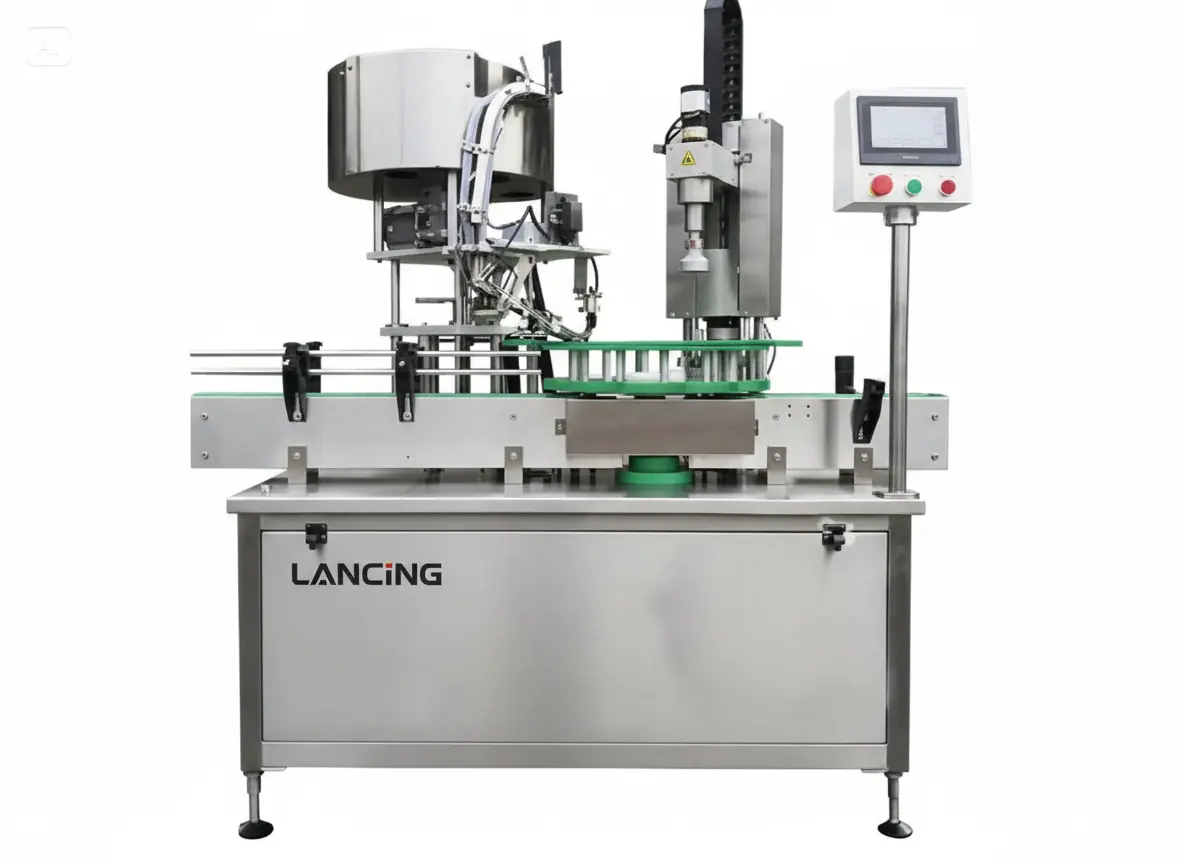
Automatic Ring Pull Crown Capping Machine
LU-XG440L crimping machine for compatible ring-pull or crown closures. Confirm cap and neck geometry, tooling and bottle support.
View machine →Automatic Servo Screw Capping Machine
Automatic servo screw capper with cap feeding, bottle clamping and conveying. Match the closure and bottle to the required configuration.
View machine →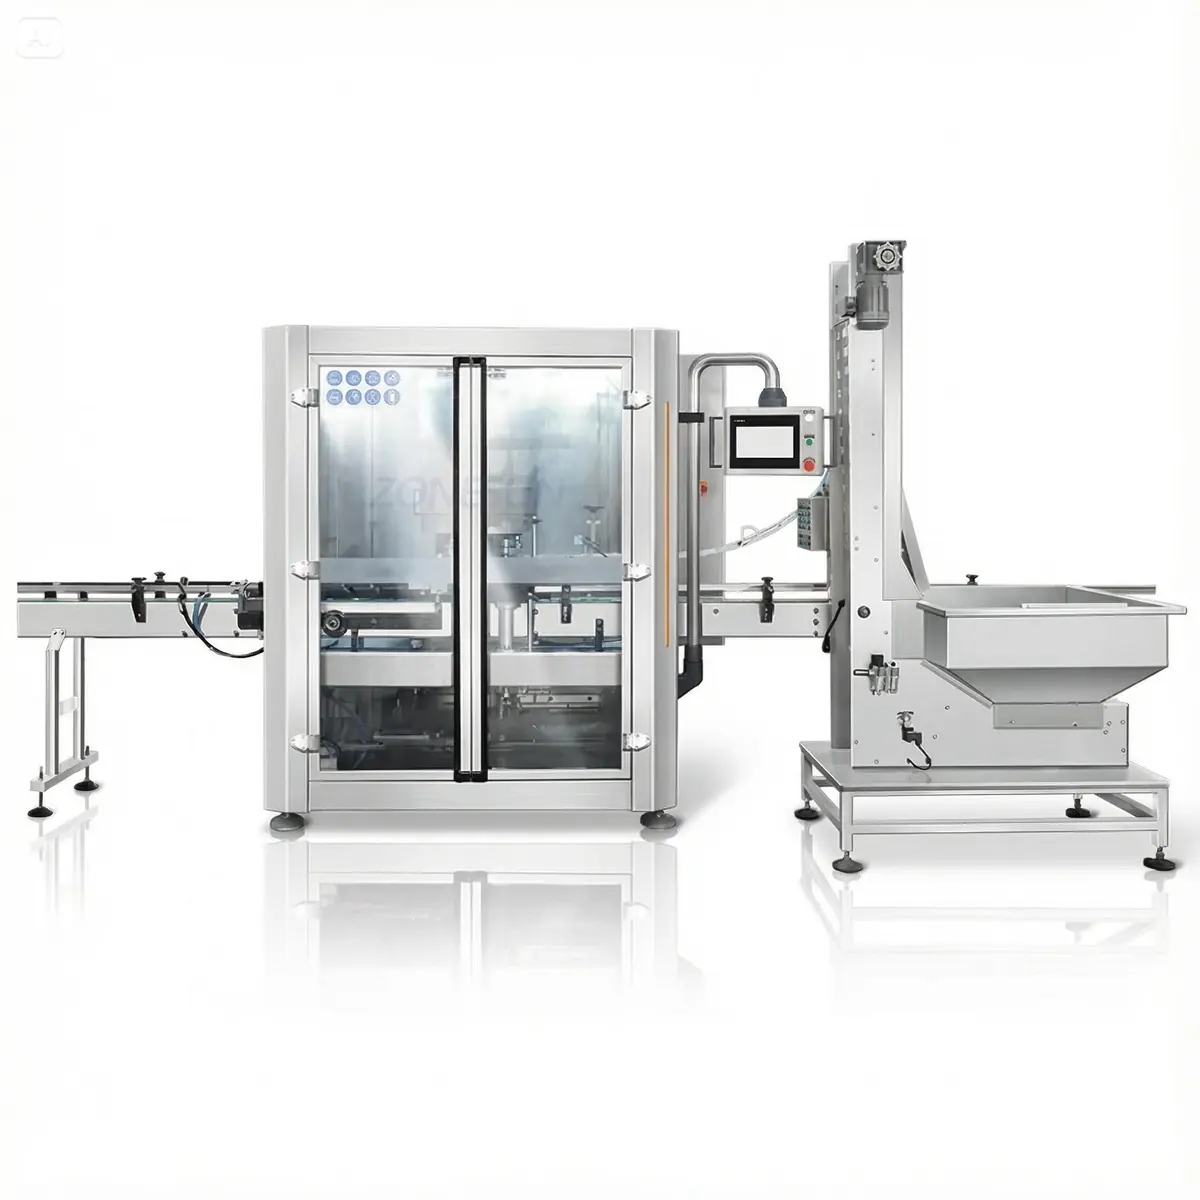
Automatic Trigger Sprayer Capper for Cleaning & Care Bottles
Trigger-sprayer capper for compatible cleaning and personal-care bottles. Confirm trigger geometry, dip-tube handling and bottle support.
View machine →LU-PVC3 Pneumatic Vial Capping Machine
LU-PVC3 pneumatic capper for compatible vial and closure formats. Confirm cap dimensions, tooling and operating requirements.
View machine →Pneumatic Perfume Bottle Capping Machine
Pneumatic perfume-bottle capper powered by an external air compressor. Confirm the bottle, closure, tooling and air requirements.
View machine →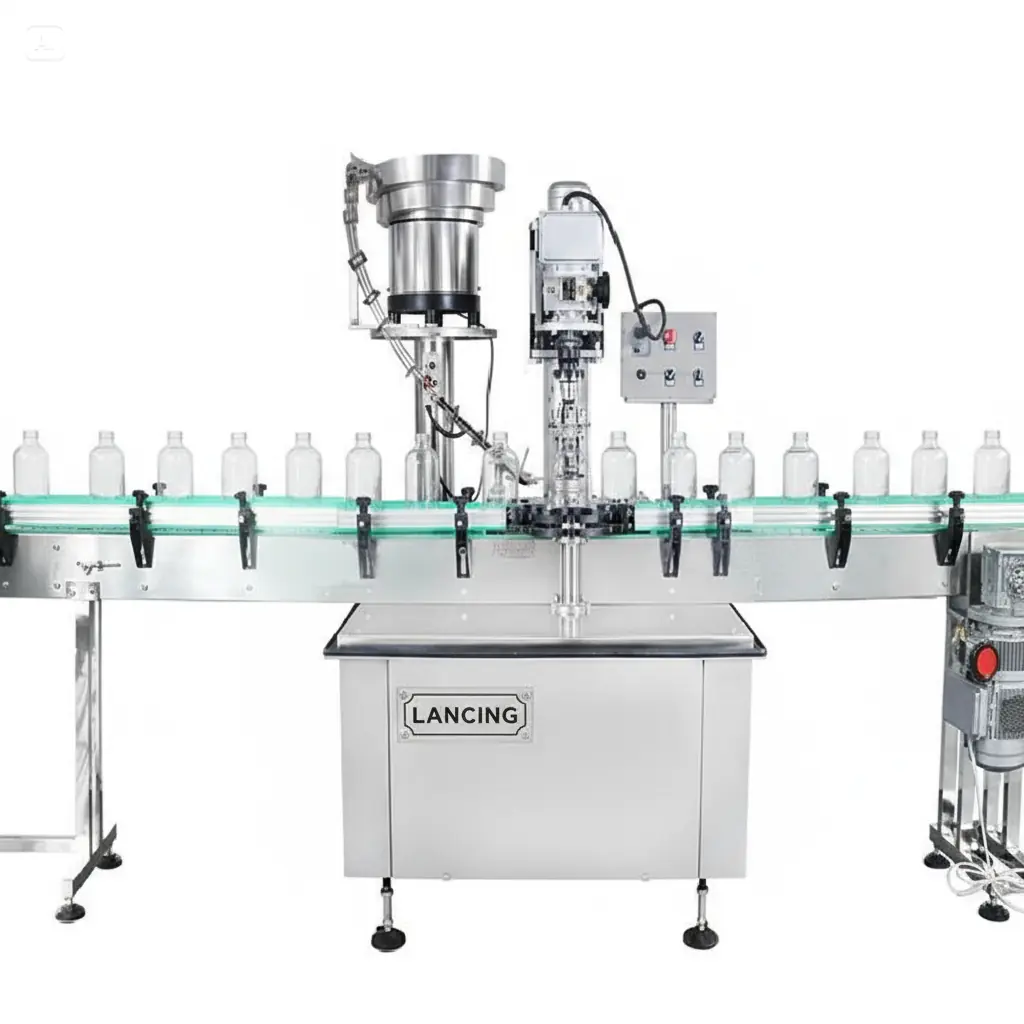
Semi Automatic Ropp Capping Machine
LU-XG60C semi-automatic ROPP capper. Match the aluminium closure, neck finish, bottle support and roller tooling.
View machine →Servo Capping Machine
LU-XG440T servo capper with a cap elevator. Confirm cap and bottle formats, required closing checks and conveyor interfaces.
View machine →What is capping machinery used for?
Capping Machinery is used to automate the relevant packaging operation as part of a standalone cell or integrated production line.
How do I specify capping machinery?
Prepare product details, pack dimensions, target output, utilities, changeover needs and any site constraints before requesting a proposal.
Can this equipment be integrated into a line?
Yes. Most projects can be combined with conveyors, coding, inspection, accumulation and end-of-line packing depending on the product and required throughput.
Choose the closure application and tightening method.
Capping performance depends on the closure, neck finish, container support, cap presentation and the quality condition that must be achieved after the cycle.
Apply, press, crimp or tighten
A closure may need placing, pressing, rolling, crimping or controlled rotation. The machine principle must match how the cap is designed to engage with the container.
Present the closure consistently
Automatic output usually depends on reliable cap orientation and delivery. Feeder selection is based on cap geometry, flexibility, surface finish and the range of formats.
Stabilise the container
Side belts, neck guides, star wheels or format tooling may be needed to resist the capping force without marking or distorting the pack.
Information to confirm before configuration
| Closure sample | Supply the cap, pump, trigger, cork, crown or ROPP component in production condition. |
|---|---|
| Neck finish | Provide representative containers and neck details, including any tolerance or supplier variation. |
| Quality target | Define torque, seating, crimp appearance, tamper evidence, leak check or another acceptance observation as applicable. |
| Feeding route | State whether closures are manually placed, bulk-fed, elevator-fed or already supplied from another unit. |
| Downstream check | Identify inspection, reject, sealing, coding and labelling processes after capping. |
Questions to resolve before selecting the closure application and tightening method.
Answers depend on the real product, packaging components and operating conditions; representative samples should be used wherever practical.
Why are cap and bottle samples needed together?
The fit, thread start, stiffness, sealing feature and tolerances act as a system; reviewing one component alone can hide compatibility problems.
Is cap feeding part of every automatic capper?
Not necessarily. The cap application unit and the feeder are separate project elements and should be defined together with the required bulk loading method.
How is tightening quality assessed?
Use an agreed check suited to the closure, such as measured removal torque, seating position, visual condition or a leak-related test.
What can cause inconsistent capping?
Variation in caps, necks, container stability, cap presentation, grip, head setting and upstream spacing can all affect the result.
Can several cap sizes run on one machine?
Potentially, but each format should be reviewed for feeder compatibility, tooling, adjustment range, change parts and practical changeover time.
Prepare a useful machinery enquiry
Send representative materials, the required output and details of any connected machinery. Lancing can then review the most suitable configuration and identify further tests or data needed.
Specify the closure, bottle and feeding method as one system.
Reliable capping depends on compatibility between the closure and neck finish, consistent component presentation, bottle support and a controlled application or tightening process.
Prove bottle and closure compatibility
Provide matched production samples, neck-finish information and details of liners, tubes, plugs, tamper-evident features or formed closures.
Choose the presentation method
Compare operator placement with bowl, elevator or other automatic feeding according to closure geometry, variation, campaign size and required orientation.
Control transfer and verification
Review bottle stability, spacing, anti-rotation, cap presence, closure quality checks and the hand-off to labelling or sealing.
Information to prepare
- Matched bottles and closures from normal supply.
- Closure dimensions, neck finish and component variation.
- Target production pattern and automation level.
- Cap presentation and replenishment method.
- Required checks for presence, position, seal or finished closure quality.
Continue from this page
Use the most relevant next step to move from initial selection towards a defined, testable project.
Bottle and closure sample trials
Test placement, tightening or forming with representative components before tooling is fixed.
Capping line controls integration
Define cap-low, blocked, starved, reject and downstream interface behaviour.
Capping project brief
Capture closure formats, output, feeding, site and acceptance requirements.
Selection and application guidance
Continue with the most relevant technical guide to compare equipment, prepare representative samples and define the line interfaces that affect final selection.
Treat the closure, container, tooling and recipe as one approved format.
Capping performance depends on the supplied closure, neck finish, presentation and bottle support. Keep physical change parts, torque or forming settings, cap-feeding behaviour and first-off checks within the controlled changeover method.